Solution for Teams
Engineering
Localize your apps, websites, and games with automated content updates by integrating with your repo
Marketing
Scale your marketing efforts through localization. Connect your marketing tools to automate the process
Support
Create and maintain multilingual support docs and other important content
Designers
Preview multilingual content, customize translations before implementation
Translators
Translate online with all the benefits of a desktop CAT tool
Use Cases
Software Translation
Set an automated process once and receive continuous localization in parallel with development
Mobile App Translation
Localize Android or iOS apps into any language and reach new markets
UI Translation
Localize your product's user interface and create global design
Website Translation
Create a multilingual website by integrating Crowdin and your website's CMS.
Multilingual Support
Translate customer service chatbots, emails, and documentation
Game Translation
Translate your game and enter the international market
E-commerce Translation
Automate localization of your e-commerce website and reach global customers.
Apps & Integrations
Browse 700+ integrations and plugins
AI Translation
Empower your business with an AI translator fine-tuned to your company's needs and get 95% publishable translations
Crowdin Resources Resources on localization services, translation and localization tipsChoosing a Chromium Carbide Overlay Plate is not a simple hardness comparison. The right choice depends on wear conditions, impact energy, temperature, and the material being handled. A plate facing fine silica dust needs a different design from one exposed to large rocks, sliding coal, or hot clinker.
Dr. John C. Lippold, a recognized welding metallurgy expert, has stated that overlay selection should follow the service environment rather than hardness alone. That principle matters here. A plate may show impressive hardness on a datasheet, yet fail early when carbide spacing, weld quality, or impact resistance is overlooked. Hardness is only one clue.
Begin with the actual failure pattern. Look at grooves, gouges, surface crumbling, and heat discoloration. Measure the worn area instead of relying on memory. Then review the plate’s alloy chemistry, carbide volume, overlay thickness, base-metal grade, and manufacturing controls. Ask for test reports, dimensional tolerances, and traceable inspection records. These details reveal more than a polished sales phrase.
There is no universal best plate.
A practical selection also considers installation. Excessive cracking can be normal in some overlays, but uncontrolled cracks, delamination, and poor fusion are warning signs. Welding procedures must suit the base material and service location. I have seen specifications become too general; that is a weakness worth admitting. Real performance depends on matching the Chromium Carbide Overlay Plate to the complete wear mechanism, not choosing the highest advertised number. This guide explains the critical questions, useful comparisons, and common mistakes before purchase.
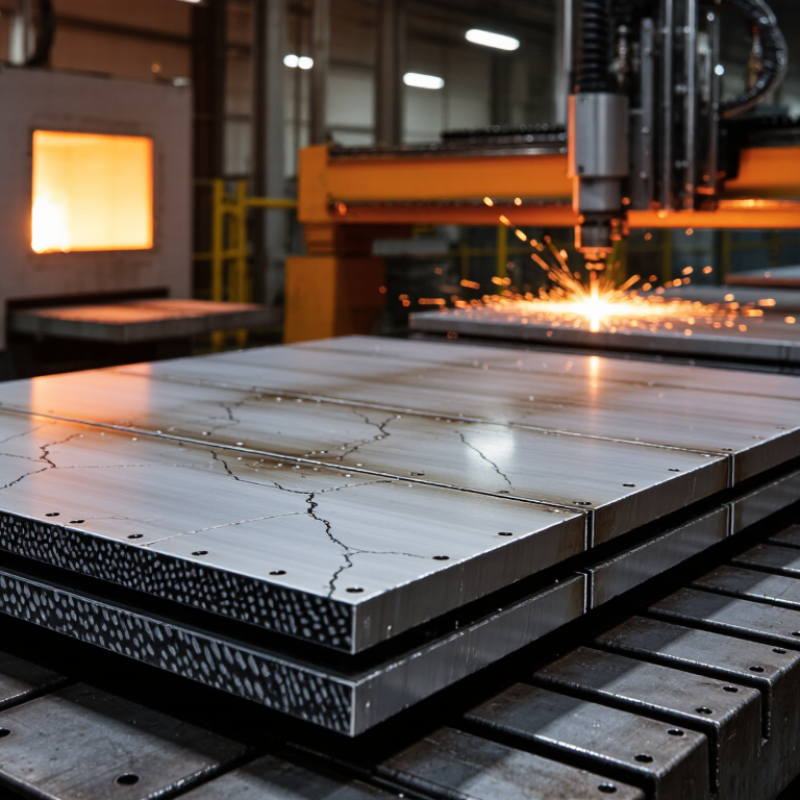
Chromium carbide overlay plate combines a tough steel backing with a hardfaced alloy layer. The backing provides structural support and helps the plate absorb impact. The overlay contains chromium-rich carbides distributed through an iron-based metallic matrix. These hard particles resist cutting, plowing, and sliding abrasion. The surrounding matrix holds them in place during service.
This structure matters in real equipment. In a transfer chute, falling ore may strike the surface and create impact damage. In a hopper, continuous sliding can remove softer metal through abrasive wear. A suitable plate must match the dominant wear pattern, not only its advertised hardness. Check overlay thickness, backing grade, surface cracking, and bond quality before installation. Controlled transverse cracks can relieve welding stress. They are not automatically defects. Excessive cracking, however, may expose weak areas.
Temperature also affects performance. High heat can soften the matrix or distort the backing. Ask for chemical analysis, hardness mapping, and ultrasonic bond inspection when reliability is critical. Measure the worn surface after service. That field evidence often improves the next selection. I have found that a thicker layer is not always better; poor fit, excessive weight, or limited weldability can reduce practical life. Some selection decisions remain imperfect without representative wear testing. Test pieces should reflect the actual material size, impact angle, moisture, and operating temperature.
Selecting a chromium carbide overlay plate starts with the wear condition, not the product name. Inspect whether the surface faces sliding abrasion, sharp impact, or both. Coal chutes often suffer from continuous sliding wear. Crusher liners may receive heavy impact from irregular rock. The difference matters. A plate designed for abrasion may crack under repeated impact. Record material hardness, particle size, flow speed, and contact pressure. Also check operating temperature and moisture. Wet, acidic materials can increase corrosion beneath the overlay.
Application requirements decide the practical specification. Measure the available space before choosing plate thickness. A thick plate may last longer, but it can reduce chute capacity or increase structural loading. Confirm cutting, drilling, bending, and welding needs with the fabricator. Site access also matters. Large sections may be difficult to install near a narrow conveyor. In my experience, wear maps are more useful than guesses. Still, field conditions are rarely uniform. A single thickness across the entire area may not be the best answer.
Tips: Mark high-wear zones after several operating weeks. Compare worn areas with the original layout. Use impact-resistant sections near drop points. Use highly abrasion-resistant sections along sliding paths. Do not ignore temperature changes. Ask for test data, hardness information, and recommended joining procedures. Poor installation can shorten service life, even when the plate selection is sound. One detail is often missed: inspect the base structure before installation. A weak support can fail before the overlay does.
Plate thickness is the first practical filter, but it should match the wear mechanism. Typical specifications separate base steel thickness from overlay thickness, such as 6+4 mm or 10+6 mm. The first value supports impact; the second resists abrasion. A thicker overlay may extend service life, yet it can increase weight, welding distortion, and replacement difficulty. Field experience suggests measuring the worn plate, not guessing from the original drawing. Small mistakes matter.
Hardness requires careful interpretation. Many chromium carbide overlays measure approximately 55–65 HRC, while ISO 6506-1 uses Brinell testing for metallic materials. These scales are not directly interchangeable. ASTM G65 testing is more useful for comparing abrasive wear, but results depend heavily on sand size, load, wheel material, and test duration. A high hardness number alone cannot predict service life. That is an uncomfortable limitation.
Microstructure often explains performance better than surface hardness. A suitable overlay commonly contains hard chromium-rich M7C3 carbides within an iron-based matrix. Published metallurgical studies frequently report carbide volume fractions near 20–40%, depending on alloy chemistry and deposition conditions. Continuous carbide networks can resist cutting, but excessive brittleness may encourage cracking. Inspect cross-sections for carbide shape, spacing, dilution, and crack direction. ASTM G65 data should be compared only under identical conditions. Real equipment remains less tidy than laboratory testing.
Choosing Chromium Carbide Overlay Plate requires more than comparing hardness numbers. Manufacturing quality should be verified through test records, not attractive certificates alone. ASTM G65 abrasion testing uses a controlled rubber wheel and silica sand system. Its standard procedure can run for 6,000 revolutions, exposing weak overlays to measurable wear. Ask for test conditions, weight loss, base-metal grade, and crack distribution. ASTM G65 results are not directly interchangeable with field performance. That detail is often overlooked.
Dimensions must match the installation drawing precisely. Check plate length, width, total thickness, overlay thickness, flatness, and hole positions. ISO 6507-1 Vickers testing can help confirm hardness consistency across the deposit. However, hardness is not toughness. A very hard surface may chip under impact. Measure several areas, especially near edges and weld terminations. A plate can pass a laboratory test and still fail because of poor fit-up. That is an uncomfortable but useful reality.
Tips: Request a dimensional inspection report before shipment. Leave practical access for lifting and welding. For large liners, consider bolted or sectional installation to reduce downtime. Welded installation may provide stronger continuity, but heat input can distort thin sections. Follow the fabricator’s approved welding procedure, and inspect the first installed panel carefully. Record gaps, cracks, and alignment. Those field notes may reveal problems that factory documents miss.
Choosing a chromium carbide overlay plate is not only a hardness decision. It is a lifecycle cost decision.
The NACE IMPACT study estimated global corrosion costs at about US$2.5 trillion annually, or 3.4% of global GDP. Abrasive wear creates a similar procurement mistake: buyers compare plate prices, but ignore shutdowns, labor, replacement parts, and lost production. A low-cost plate can become expensive within weeks. In cement, mining, and steel plants, I would request ASTM G65 abrasion results, chemical analysis, hardness mapping, overlay thickness, and welding guidance. One hardness value is not enough. Uneven carbide distribution may leave soft zones beside heavily protected areas.
Ask suppliers for traceable batch records and recent third-party test reports. ISO 9001 certification supports process control, but it does not prove field performance. Confirm the test method, sample location, and acceptance limits. Also inspect flatness and crack patterns before installation. Controlled stress-relief cracks can be normal in overlays, yet excessive cracking needs technical review.
Build a simple cost model: purchase price, cutting and fitting, installation hours, expected service months, and production losses. Then compare cost per operating hour. A plate lasting 14 months may outperform one lasting six months, even with a higher initial price. The spreadsheet often lies. Field conditions change. Feed size, impact angle, moisture, and welding quality can overturn laboratory results, so request references from similar applications and review actual replacement records.
| Evaluation Dimension | Typical Technical Benchmark | What to Confirm with the Supplier | Lifecycle Cost or Reliability Impact |
|---|---|---|---|
| 1. Application and Wear Mechanism | |||
| Primary wear type | CCO plate is mainly suitable for severe abrasive wear caused by sliding or impact from materials such as ore, coal, clinker, sand, and cement raw materials. | Request an application review covering material hardness, particle size, impact energy, operating temperature, moisture, and corrosive chemicals. | Correctly matching the wear mechanism can reduce premature replacement and avoid paying for an unnecessarily expensive alloy. |
| Operating temperature | Many conventional CCO products are used continuously below approximately 400°C. Higher-temperature service requires confirmation of alloy stability, base plate performance, and welding procedure. | Obtain the supplier’s documented maximum continuous and intermittent service temperatures for the proposed grade and thickness. | A temperature mismatch can cause cracking, distortion, loss of hardness, or rapid wear, increasing downtime and replacement cost. |
| 2. Overlay Metallurgy and Hardness | |||
| Chromium content | Typical chromium content in common hypereutectic CCO deposits is approximately 20–30% by mass. | Review the chemical analysis or heat/production-batch certificate. Confirm whether the reported values refer to the overlay deposit rather than only the welding consumable. | Higher chromium content does not automatically provide longer life; the complete alloy system and wear mechanism must be considered. |
| Carbon content | Typical carbon content is approximately 4–5% by mass in many standard chromium-carbide overlay deposits. | Request a certificate showing actual chemical composition and permitted tolerances for every production batch. | Carbon and chromium control affects carbide formation, hardness, crack pattern, weldability, and service life. |
| Overlay hardness | A common target range is approximately 55–65 HRC, although test method, location, dilution, and alloy grade affect the result. | Confirm the test standard, sampling location, number of readings, minimum acceptable value, and whether hardness is measured on the deposit surface or cross-section. | A higher hardness value alone is not sufficient; excessive brittleness may increase spalling under impact conditions. |
| Hard-phase structure | Typical CCO microstructures contain chromium-rich carbides distributed in an iron-based matrix. Carbide morphology and distribution influence wear resistance. | Ask for representative metallographic images and a description of carbide distribution, matrix condition, and dilution control. | Uniform hard-phase distribution generally supports more predictable wear and reduces localized failure. |
| 3. Plate Construction and Dimensional Control | |||
| Overlay thickness | Common overlay thicknesses range from approximately 3 to 20 mm, depending on wear allowance and plate construction. | Confirm nominal thickness, minimum local thickness, measurement method, and allowable tolerance after welding and finishing. | An excessively thick overlay increases weight and purchase cost; an undersized overlay may shorten replacement intervals. |
| Base plate thickness | Base plate thickness commonly ranges from approximately 4 to 20 mm and provides structural support and weldability. | Confirm base material grade, yield strength, thickness tolerance, and compatibility with the equipment structure. | An unsuitable base plate can cause distortion, cracking, installation difficulty, or structural failure. |
| Plate dimensions | Large-format plates are often manufactured around 1,500 × 3,000 mm, 1,500 × 6,000 mm, or according to approved drawings. | Confirm maximum production size, cut-part accuracy, edge condition, flatness, hole tolerances, and drawing revision control. | Accurate dimensions reduce site cutting, welding, fitting time, material waste, and installation downtime. |
| Surface and edge condition | The wear surface should be free from harmful slag, loose defects, and unfilled areas. Overlay plates commonly show transverse checking cracks caused by weld-deposit shrinkage. | Confirm the accepted crack pattern, maximum crack width or length if specified, defect repair procedure, and edge finishing requirements. | Clear acceptance criteria prevent disputes and reduce the risk of installing defective or difficult-to-weld parts. |
| 4. Supplier Reliability and Quality Assurance | |||
| Traceability | Each plate or production batch should be traceable to raw materials, welding parameters, inspection results, and shipment records. | Require heat number, batch number, production date, plate identification, inspection record, and material certificate. | Traceability simplifies root-cause analysis, warranty claims, repeat orders, and quality audits. |
| Inspection documentation | A robust quality package may include chemical analysis, hardness results, dimensional inspection, visual inspection, and repair records where applicable. | Agree on inspection and test plans before production, including sampling frequency and acceptance criteria. | Documented inspection lowers the probability of receiving nonconforming material and reduces rework costs. |
| Production process control | Consistent welding speed, current, voltage, heat input, interpass temperature, and consumable control are important for repeatable overlay quality. | Request a process description, welding procedure qualification where applicable, calibration records, and operator qualification information. | Stable process control improves batch-to-batch consistency and makes service-life estimates more reliable. |
| Sample approval | A production sample or first-article inspection is recommended for critical wear parts and complex cut-and-formed components. | Approve a representative sample for chemistry, hardness, thickness, dimensions, weldability, and appearance before full production. | Early validation is usually less expensive than correcting a full shipment that does not fit or perform as expected. |
| Technical support | A capable supplier should provide cutting, forming, welding, installation, storage, and maintenance guidance. | Confirm response time, engineering contact, repair recommendations, installation drawings, and field-support scope. | Good technical support can reduce installation errors, unplanned shutdowns, and premature damage. |
| 5. Total Lifecycle Cost Calculation | |||
| Initial purchase cost | Include plate price, cutting, drilling, forming, packaging, freight, import charges, and applicable taxes. | Request a fully itemized quotation based on the final drawing, quantity, delivery term, inspection level, and packaging requirement. | Initial cost = material + processing + inspection + logistics + taxes |
| Installation cost | Include removal of old liners, lifting, fitting, welding, consumables, scaffolding, and post-installation inspection. | Ask for estimated labor hours, recommended welding consumables, preheat requirements, and installation method. | Installation cost = labor hours × labor rate + equipment + consumables |
| Production downtime | Downtime cost depends on lost production, labor, restart procedures, and downstream disruption. | Estimate planned replacement hours and compare them with the expected service interval of each approved option. | Downtime cost = outage hours × production loss per hour |
| Maintenance and repair | Include inspection, patch welding, crack repair, surface preparation, and replacement of associated fasteners or supports. | Confirm whether the overlay can be repaired in service and which welding procedure is approved for maintenance. | Maintenance cost = inspection + repair labor + repair materials + access equipment |
| Expected service life | Use measured wear data from comparable operating conditions whenever possible. Avoid relying only on laboratory abrasion rankings. | Request references for similar material flow, impact level, temperature, plate thickness, and operating hours. | A lower purchase price may produce a higher annual cost if the replacement interval is shorter. |
| Annualized lifecycle cost | Compare alternatives over the same evaluation period and use consistent assumptions for production loss and maintenance. | Document all assumptions and perform a sensitivity analysis for service life, downtime rate, freight, and labor cost. | Annualized cost = (purchase + installation + downtime + maintenance) ÷ expected service life in years |
| 6. Decision Rules | |||
| Recommended approval status | Approve when technical requirements, inspection documents, dimensions, delivery, and lifecycle assumptions are all verified. | Use a signed technical data sheet and approved drawing as the purchasing reference. | Reduces technical ambiguity and protects the expected service-life calculation. |
| Conditional approval | Conditional when the price is attractive but test records, traceability, or application evidence are incomplete. | Require additional samples, third-party testing, or a controlled trial before applying the product to critical equipment. | Controls risk while allowing qualification of a potentially competitive source. |
| Reject or re-quote | Reject when chemistry, hardness, thickness, dimensions, warranty terms, or inspection requirements cannot be documented. | Do not compare quotations on price alone; request a technically equivalent offer or revise the specification. | Avoids hidden costs caused by poor fit, early wear, rework, emergency freight, and unplanned downtime. |
Crowdin has been translated by volunteers, and some translations might be incomplete. You can help us translate Crowdin into your language by adding new translations or voting for existing ones.
Contribute language Global website